

User-first overview
You the specifier or production lead need solutions that actually work on the shopfloor, lah. This guide focuses on practical steps for scaling throughput on wholesale automated assembly lines, anchored in real show-floor learnings from Medtec events — see the medical device manufacturing trade shows link for context — and prioritises what matters to your operators, quality team and procurement folks. Expect straight advice about assembly line automation, cleanroom classification and process validation so you can decide fast and safely.
Where teams trip up during scale-up
Most problems start not with tech, but with mismatch: equipment speed vs human takt time, or an automated station that needs a cleaner environment than the existing cleanroom can supply. Common mistakes include pushing robot cycles faster without validating upstream buffer handling, ignoring sterile packaging constraints, and skipping small-sample validation runs. These lead to rework, increased scrap rates and delayed product release — costly one-shot errors that kill momentum.
Practical, stepwise approach
Start by mapping the flow from component receipt to final inspection. Break the line into measurable segments: pick-and-place throughput, cure or sterilisation dwell time, inspection station cycle time. Use time studies and short pilot runs to set realistic cycle targets. Then match equipment: swapping a manual station for a robotic pick-and-place cell helps only if upstream feeders and downstream conveyors are balanced. Validation must be staged — first functionality, then environmental, then full process validation — so you don’t waste time on repeat trials.
Design choices that actually scale
Choose modular automation cells over monolithic systems when volume projections have wide variance. Modular cells let you add another pick-and-place or inspection camera without tearing the whole line apart. Standardise tooling interfaces so changeovers take minutes, not hours. Invest in localised environmental controls rather than upgrading the entire cleanroom if the issue is limited to a single station — that saves cost and reduces qualification complexity.
Operator-centred controls and handover
Automation not meant to replace operators — it should empower them. Provide intuitive HMI screens with clear error recovery steps and rapid fault logging. Include physical aids: jigs, poka-yoke guides, and simple audible prompts for cycle completion. Train supervisors on basic PLC troubleshooting so small hiccups get fixed quickly, and use digital logs to spot recurring failure modes for targeted improvement.
Lessons from the trade floor — real anchor
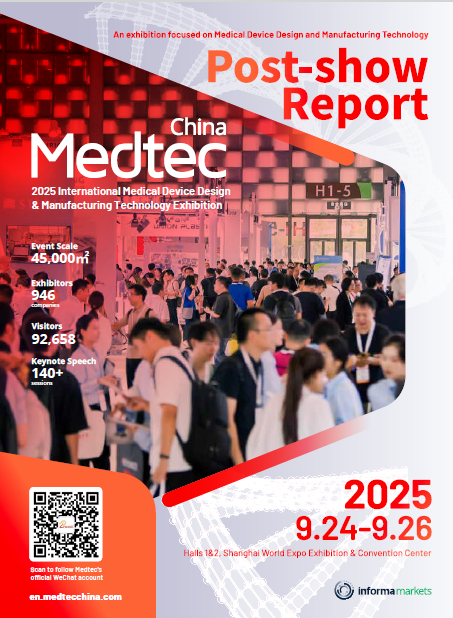
At Medtec China in Shanghai, vendors showed low-footprint automation that solved specific bottlenecks instead of selling whole-line upgrades — that real-world demo helped teams select modular solutions faster. Seeing a cell run in a live environment clarified throughput claims versus lab numbers, and vendors who brought validation data won trust quickly. These on-site demos are good for benchmarking parts per minute against real workloads, not just spec sheets.
Common pitfalls and how to avoid them
Avoid these: underestimating spare-part lead times, mixing incompatible communication protocols across PLCs, and skipping environmental stress runs. Do a quick risk matrix for each new cell: failure impact, detection time, and recovery steps. Keep spare components for high-failure items and standardise on a small set of communication protocols to reduce integration headaches — saves you months of debugging later.
Advisory — three golden rules for selection and evaluation
1) Throughput authentication: verify vendor throughput using onsite pilot runs under your product mix, not generic demos. Track yield, cycle time and mean time between failures.
2) Integration readiness: demand clear I/O and communication specs, and a plan for conveyor, vision and MES integration. Confirm compatibility with your existing PLCs and data historians.
3) Validation footprint: require a staged validation plan covering functionality, environmental control and full process validation with documented acceptance criteria — that way commissioning doesn’t stall at QA sign-off.
Final thought — Medtec events consistently show that practical, modular automation wins over one-size-fits-all systems; pick solutions that match your real constraints and scale by adding repeatable cells, not ripping everything out. — Medtec.

